

ESBR Process Optimization: Cost Reduction, Capacity Improvement and Product Differentiation
SUMMARY
Existing ESBR plants are facing increasing competitive pressure from global overcapacity, particularly in China, and the continuing shift toward SSBR in high-performance tire applications. To remain competitive, ESBR producers must reduce production costs, improve environmental performance by lowering energy consumption, emissions and effluents, and/or differentiate their product portfolio toward specialty and higher-value applications. Innventik’s integrated process-assessment methodology evaluates the complete ESBR production chain to identify and prioritize opportunities for cost reduction, debottlenecking, sustainability improvement and product differentiation.
Emulsion Styrene-Butadiene Rubber (ESBR) remains one of the most established synthetic rubber technologies in the industry. Although the fundamental process has been used commercially for many decades, significant opportunities remain to improve the economics, reliability, environmental performance and product capabilities of existing ESBR plants.
For many producers, the objective is not to replace an established process. It is to identify where value is being lost within the existing plant and determine which process, operational and technological improvements can deliver measurable benefits.
At the same time, the competitive position of conventional ESBR assets is becoming increasingly challenging. Global synthetic-rubber capacity, particularly the continued expansion of production in China, is intensifying cost and margin pressure. In the tire sector, the long-term shift from ESBR toward SSBR and SSBR-Functionalized grades for high-performance applications is also a reality, driven by increasingly demanding requirements for low rolling resistance, wet grip and energy efficiency. This trend is particularly relevant for premium and EV tires, where advanced and functionalized SSBR grades are increasingly important.
Under these conditions, existing ESBR plants need a clear strategy to remain competitive: Become more cost-efficient; reduce their environmental footprint through lower energy consumption, emissions, water use and effluent generation; and/or differentiate their product portfolio by moving toward novel, specialty and higher-value applications. Assets unable to improve their cost position or create differentiated value will face increasing pressure for rationalization or eventual closure.
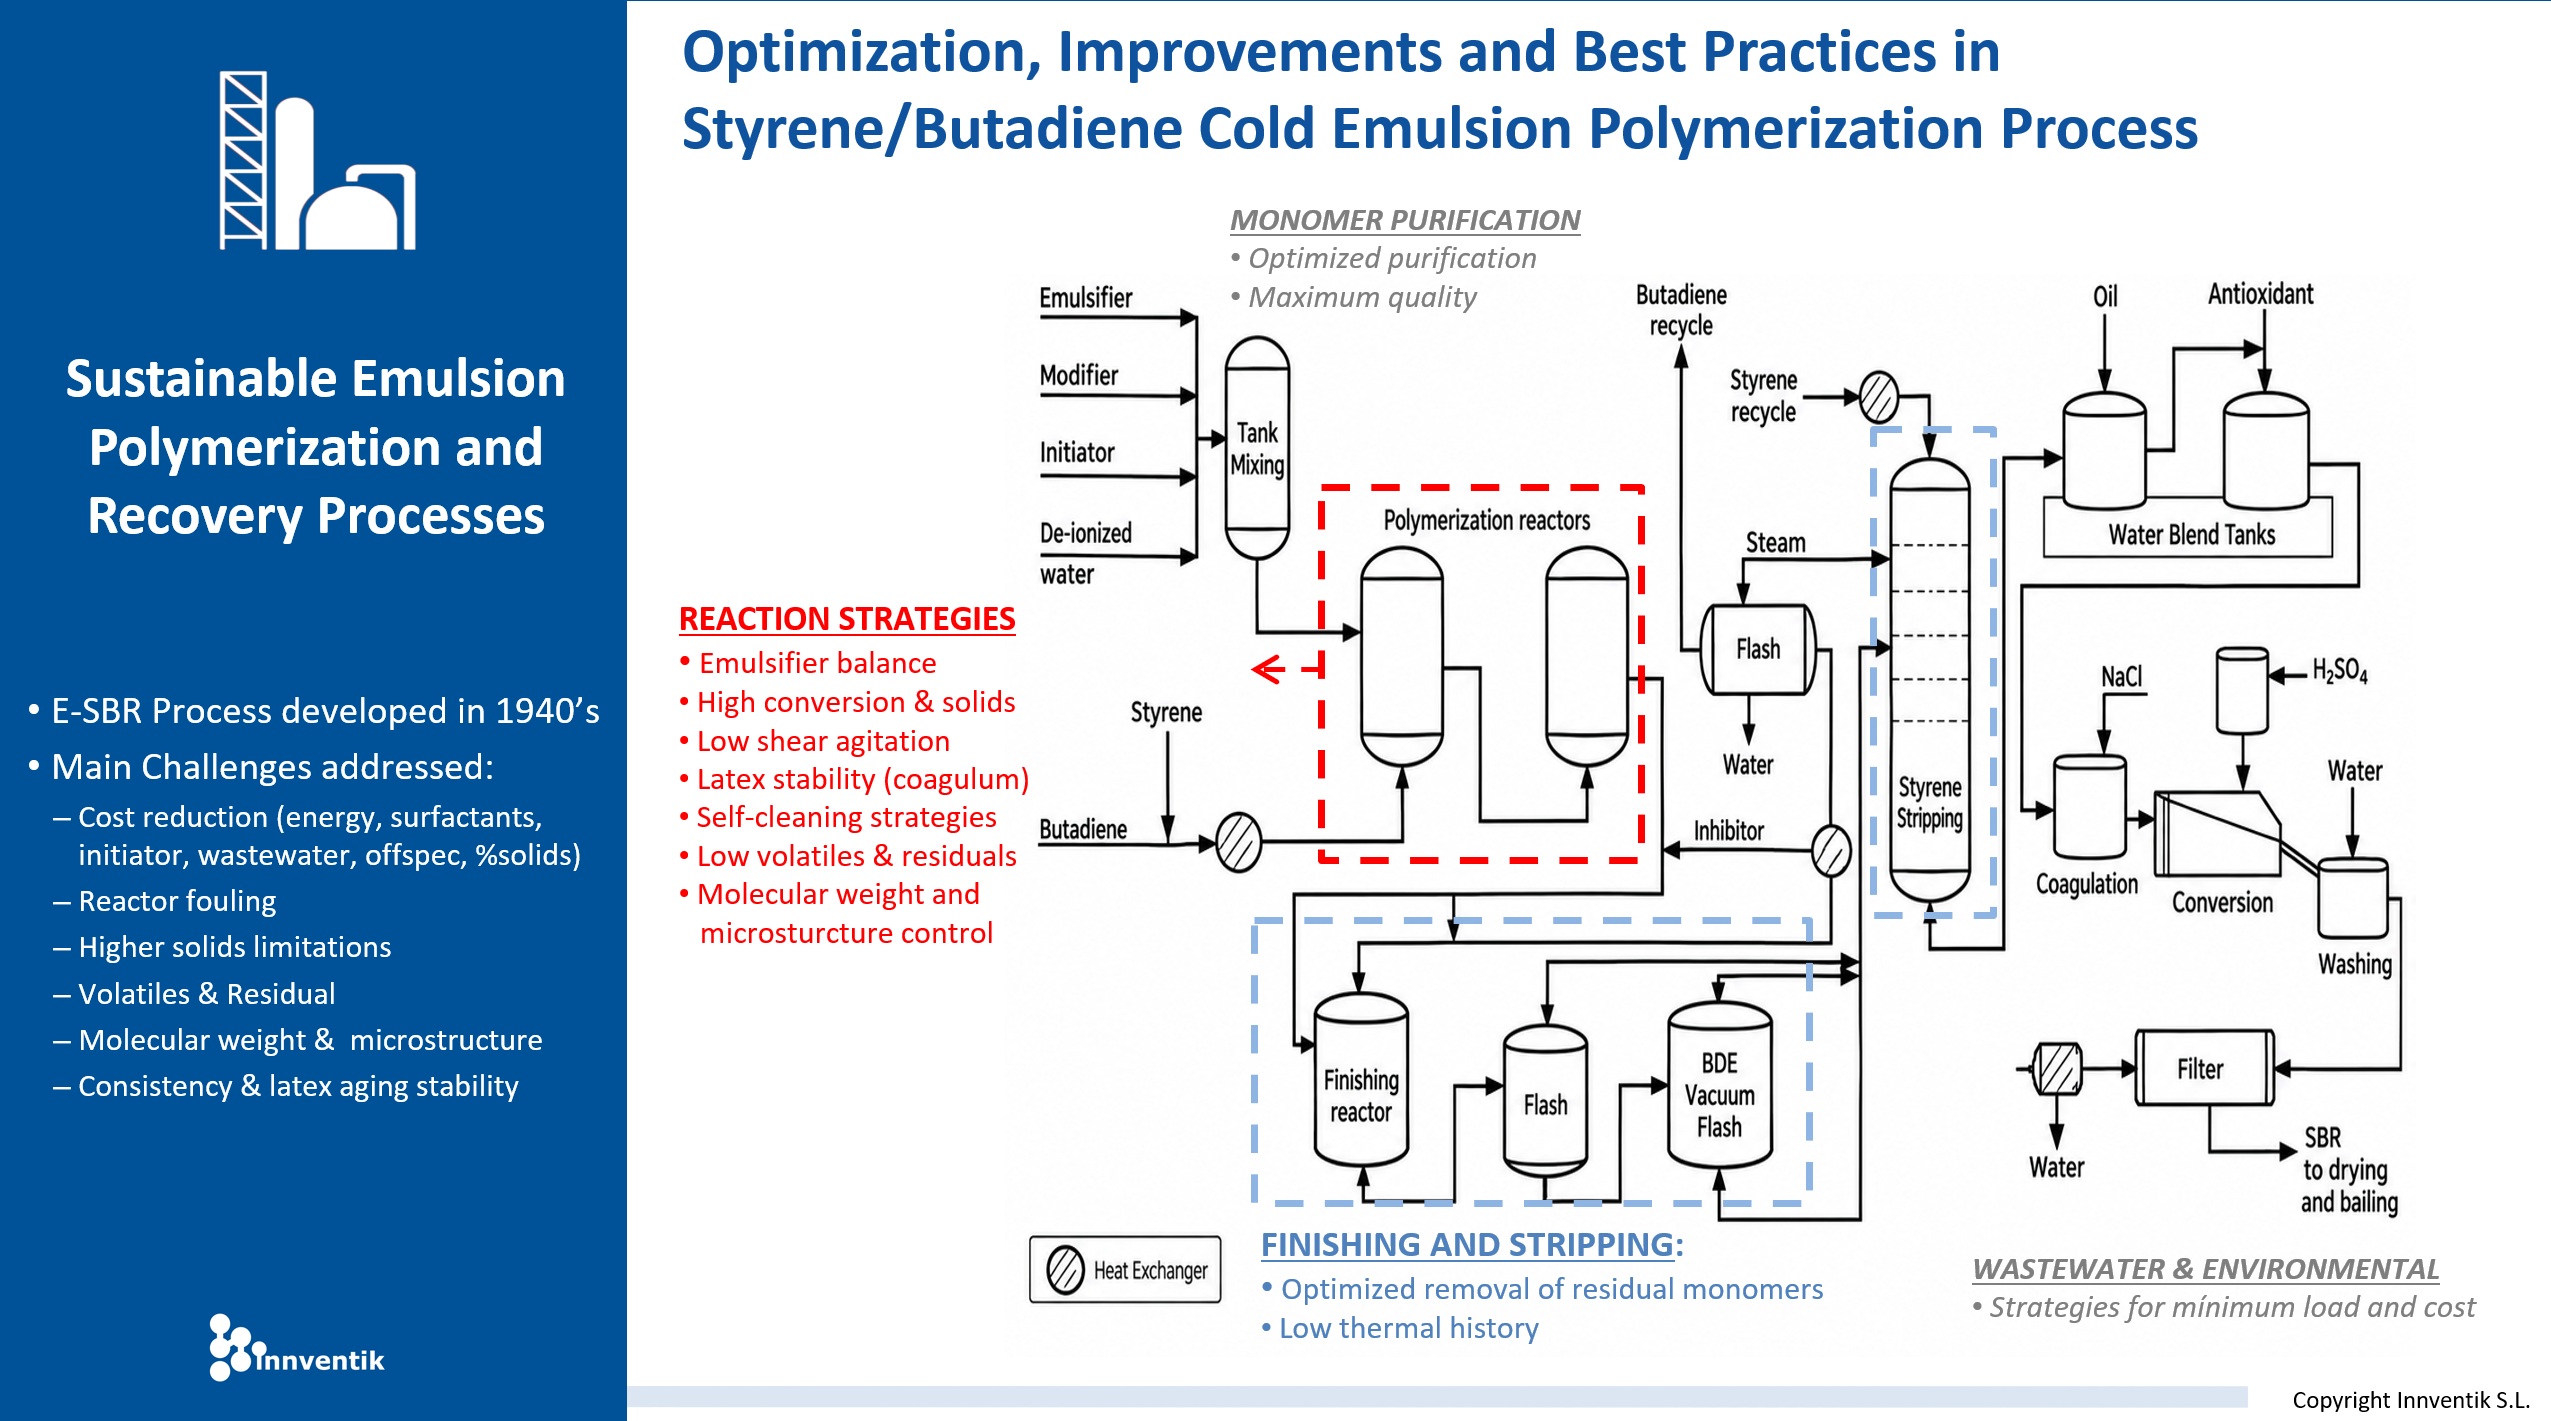
An effective ESBR optimization program should therefore address the complete production chain—from raw-material preparation and polymerization through monomer recovery, coagulation, dewatering, drying and finishing—while considering the interactions between these operations. Key areas include emulsifier balance, conversion and solids, agitation, latex stability, fouling, residual monomers, monomer purification, stripping and finishing, and wastewater management.
The objective is straightforward: produce more consistently, at lower cost, with existing assets whenever possible, while creating the flexibility required to manufacture differentiated and higher-value grades.
Where is value typically lost in an ESBR plant?
The first step in process optimization is not immediately proposing new equipment or technology. It is identifying the actual constraints of the plant. Typical questions include: What is the plant’s critical bottleneck? What percentage of production is off-specification, downgraded or reprocessed? What prevents operation at higher conversion or higher solids? Which operation has the greatest impact on production cost or capacity? Where can product differentiation generate additional value?
The answers are rarely associated with a single unit operation. Monomer purification and recovery, Polymerization kinetics, heat removal, fouling, latex stability, residual monomer removal, coagulation behavior and finishing capacity are interconnected. Improving one area without considering its effect on downstream operations can simply move the bottleneck elsewhere. For this reason, process optimization should evaluate the plant as an integrated system and distinguish between the different mechanisms through which value can be created.
A structured framework for process optimization and cost reduction
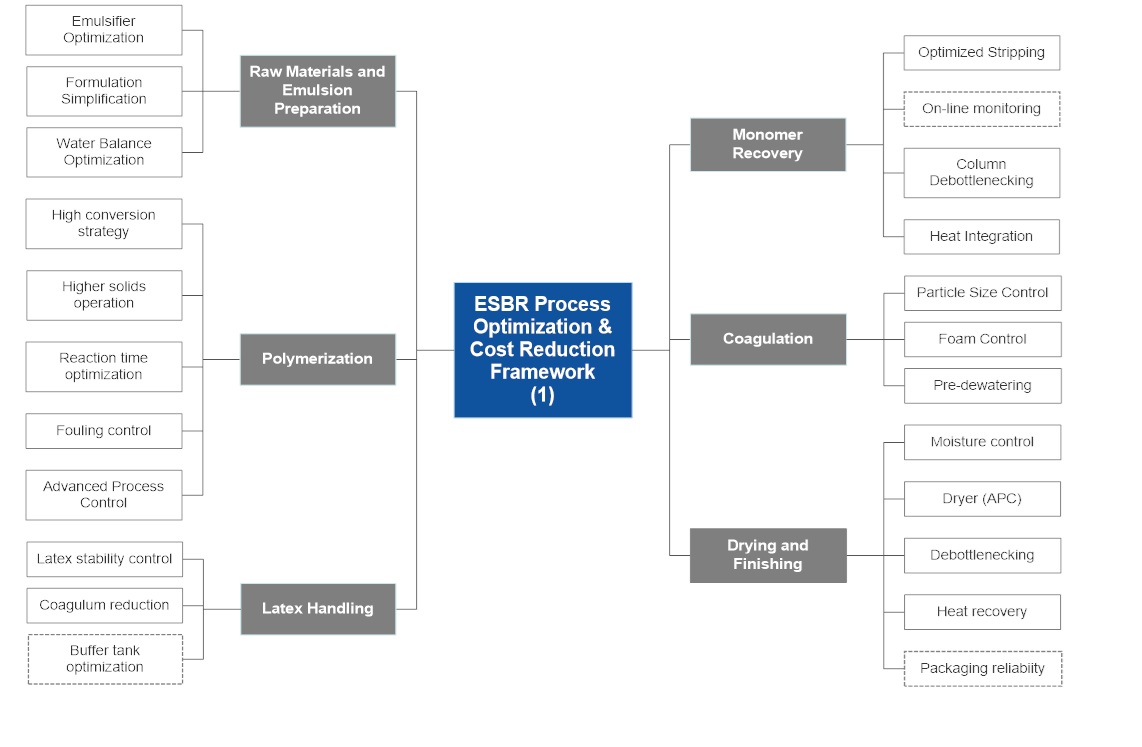
ESBR process optimization begins with understanding how the individual operating variables and unit operations affect overall plant performance. The objective is to identify improvement opportunities systematically rather than addressing individual symptoms in isolation. The optimization framework considers the relationships between polymerization performance, operating stability, capacity utilization, raw-material efficiency, utilities, recovery and downstream processing. This allows technical opportunities to be linked to specific economic objectives such as increased production, reduced variable cost, lower off-specification generation or improved plant availability.
The first group of opportunities is associated directly with the polymerization section, where batch cycle, conversion, reactor utilization, heat removal, fouling and process variability can determine both capacity and manufacturing cost.
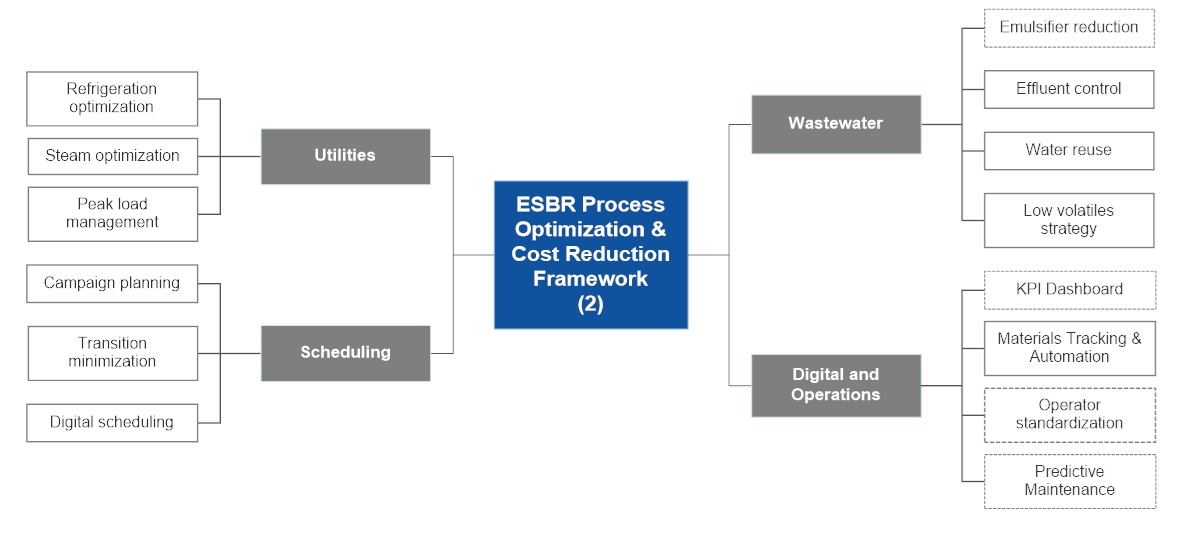
Optimization should not stop at polymerization. Monomer recovery, refrigeration and energy systems, coagulation, dewatering, drying and finishing can become equally important constraints.
This second level of analysis is particularly important when upstream improvements increase production. Additional polymerization capacity has limited economic value if monomer recovery or finishing subsequently becomes the bottleneck.
The complete process must therefore be evaluated as an interconnected production system, identifying where changes in one area affect capacity, energy consumption, product losses, quality or operating stability elsewhere.
Key opportunities for ESBR process optimization
Several areas repeatedly offer opportunities for improvement in established ESBR plants. These include batch-cycle optimization, conversion improvement, higher solids, fouling reduction, heat-removal optimization, monomer recovery, energy integration, coagulation efficiency, drying and finishing debottlenecking, grade-transition optimization and new-grade development.
Polymerization cycle and reactor utilization
Batch-cycle optimization can directly increase effective plant capacity without installing additional polymerization reactors. The analysis should identify the individual contributions to total batch time and distinguish necessary reaction time from waiting, preparation, transfer and other non-productive periods. Cycle-to-cycle variability is equally important: reducing average cycle time provides limited benefit if process variability prevents consistent scheduling and reactor utilization. Optimization therefore involves both cycle-time reduction and cycle consistency.
Conversion, solids and polymerization stability
Increasing conversion can reduce residual monomer loads and improve plant productivity. Higher solids can also increase effective capacity and reduce the amount of water handled downstream. However, these improvements cannot be pursued independently of latex stability, heat removal and fouling. The polymerization system must maintain the appropriate balance between emulsifier chemistry, initiation system, agitation, heat transfer and reaction kinetics. Higher conversion or solids becomes economically attractive only when it can be achieved without unacceptable increases in coagulum, reactor fouling, instability or batch variability.
Reactor fouling and heat removal
Reactor fouling has consequences beyond cleaning costs. Deposits progressively reduce heat-transfer performance, potentially increasing batch time, affecting temperature control and contributing to variability between campaigns. Cleaning requirements also reduce plant availability. Consequently, fouling should be evaluated together with reactor hydrodynamics, heat-transfer performance, cooling/brine control, recipe conditions and latex stability rather than treated exclusively as a maintenance issue.
Raw-material and monomer quality
Polymerization performance begins upstream of the reactor. Variations in monomer, water, emulsifier and initiator quality can influence reaction rate, conversion, latex stability and overall process consistency. Purification requirements and recycle streams therefore need to be considered as part of the polymerization system. The objective is not necessarily maximum purification everywhere, but consistent raw-material quality appropriate for stable polymerization and the required final-product specifications.
Monomer recovery and stripping
Residual styrene and butadiene represent both a product-quality issue and an economic loss. Optimization of flash and stripping operations can improve monomer recovery while reducing energy requirements and stabilizing recycle-stream quality. The interaction between conversion and recovery is particularly important: polymerization conditions determine the residual-monomer load that the recovery section must subsequently process. An integrated assessment should therefore consider polymerization conversion, stripping efficiency, recycle purity and energy consumption together rather than as independent optimization problems.
Coagulation, water management and finishing
Coagulation strongly influences downstream equipment performance. Variability in crumb formation, particle size or foaming can affect washing, dewatering and drying. Poor coagulation performance may consequently appear downstream as excessive moisture, dryer limitations or unstable finishing operation. Finishing can also become the effective capacity limitation when upstream production is increased. Moisture variability, insufficient dewatering, dryer efficiency and frequent interruptions can restrict throughput even when polymerization capacity is available. The correct approach is therefore to evaluate coagulation, dewatering and drying as an integrated system.
Energy integration
ESBR production requires significant refrigeration, steam and other utilities. Energy optimization should therefore extend beyond individual equipment efficiencies. Particular attention should be given to refrigeration systems, heat integration, steam consumption and the relationship between operating conditions and utility demand. Historical plant data can be used to establish specific energy consumption against production rate and grade and determine whether utility systems themselves constrain production.
Cost reduction is only part of the opportunity
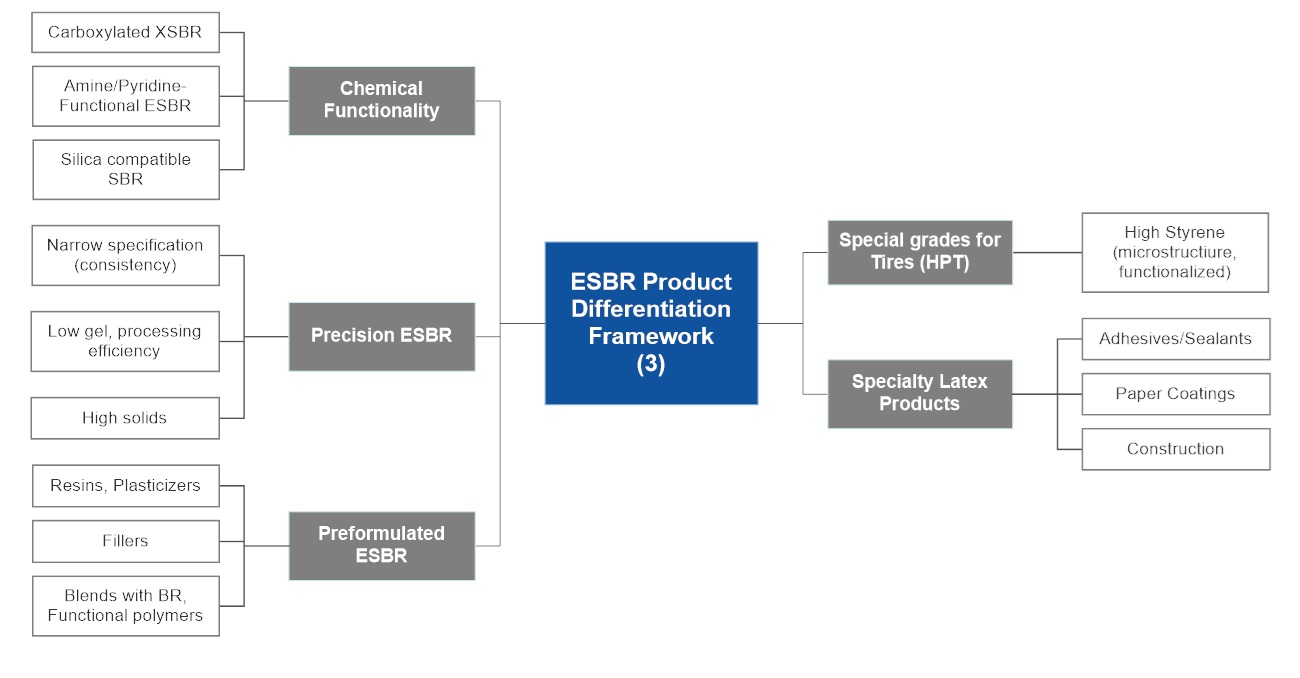
Optimization programs frequently begin with a cost or capacity objective. However, an established ESBR plant can also be evaluated from a product-differentiation perspective.Once the process operates consistently, the same understanding of polymerization chemistry, molecular-weight control, microstructure, emulsifier systems, conversion and finishing can be applied to determine whether the plant can manufacture grades targeted at more demanding or higher-value applications. This changes the question from:
“How can we manufacture the existing grades more cheaply?”
to:
“What additional products can this asset manufacture competitively?”
Potential differentiation must be evaluated against the real capabilities of the existing polymerization and finishing systems. In some cases, modifications to recipes and operating conditions may be sufficient. In others, targeted process modifications may be required. The important point is that process optimization and product development should not necessarily be treated as separate activities. Improved process control and consistency can create the operating window required for new product development.
From process optimization to measurable business value
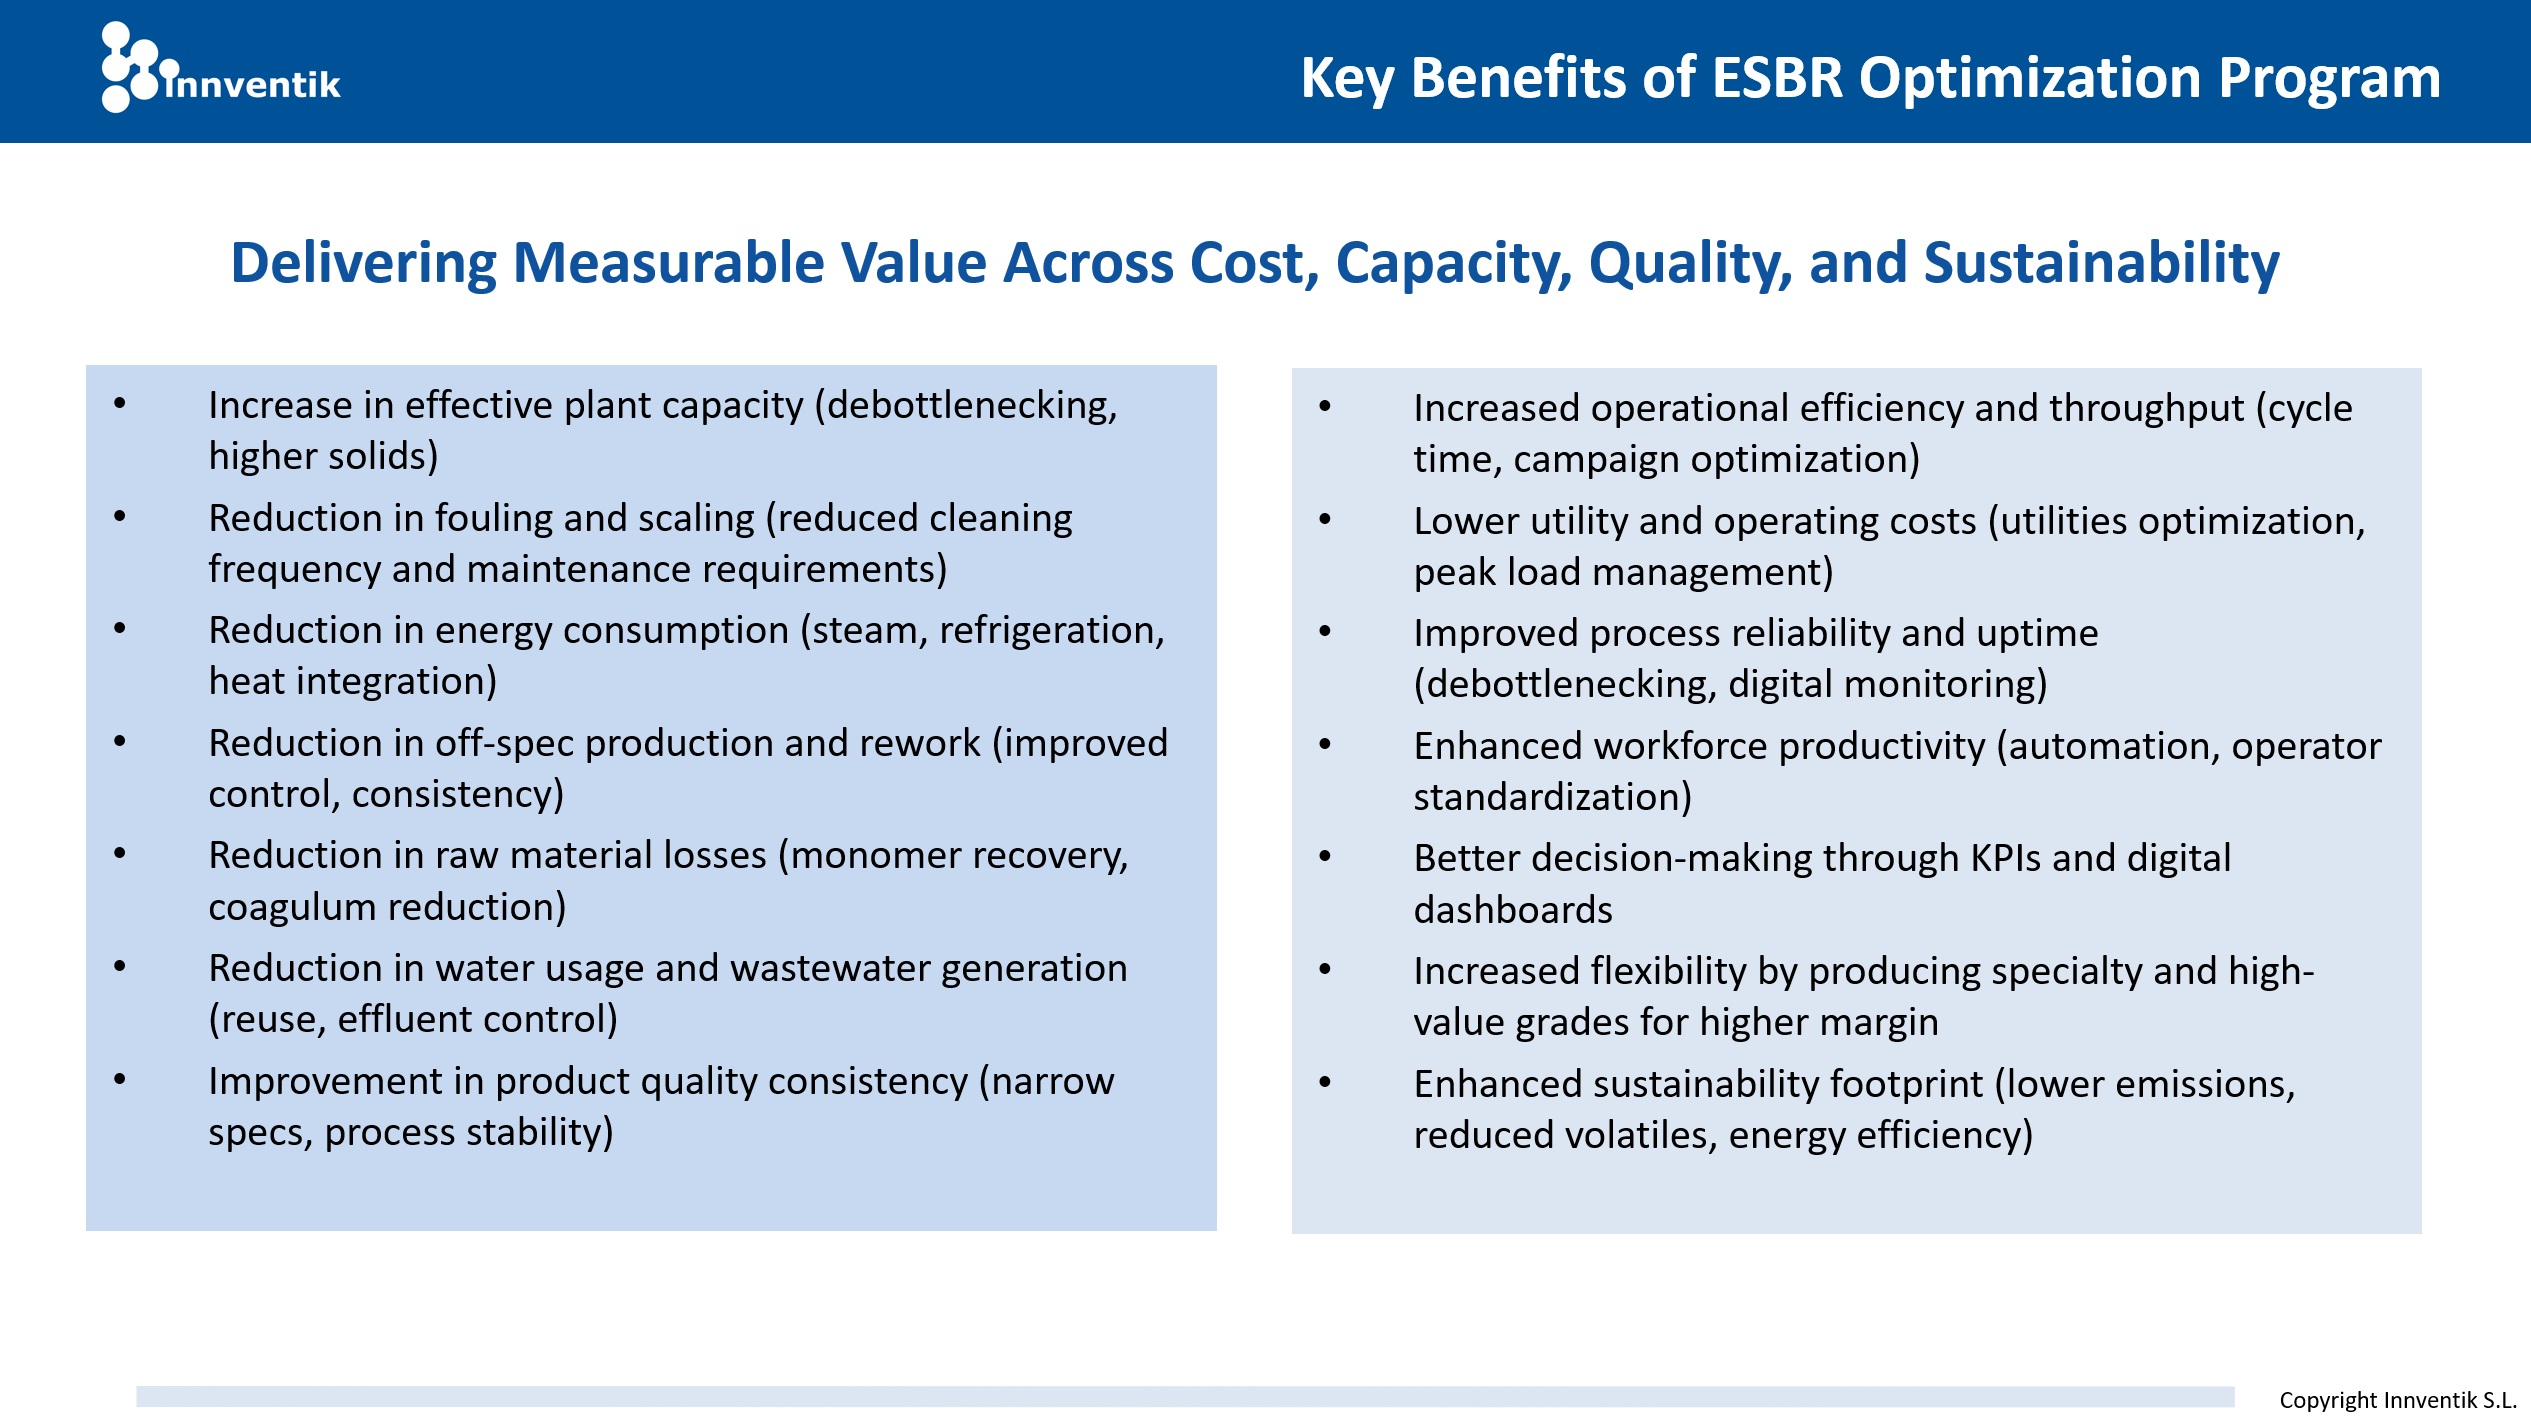
The purpose of the assessment is not simply to identify technically interesting improvements. Each opportunity should ultimately be translated into operational and economic value. Depending on the plant, potential benefits include increased effective production capacity through debottlenecking and higher solids; reduced fouling, cleaning frequency and maintenance; lower steam and refrigeration consumption; reduced off-specification production and rework; lower raw-material and monomer losses; reduced water consumption and wastewater generation; improved product consistency; increased reliability and uptime; greater workforce productivity; and increased flexibility to manufacture specialty and higher-value grades.
The objective is therefore to move from individual technical observations to measurable value across cost, capacity, quality and sustainability.
A structured ESBR Process Assessment
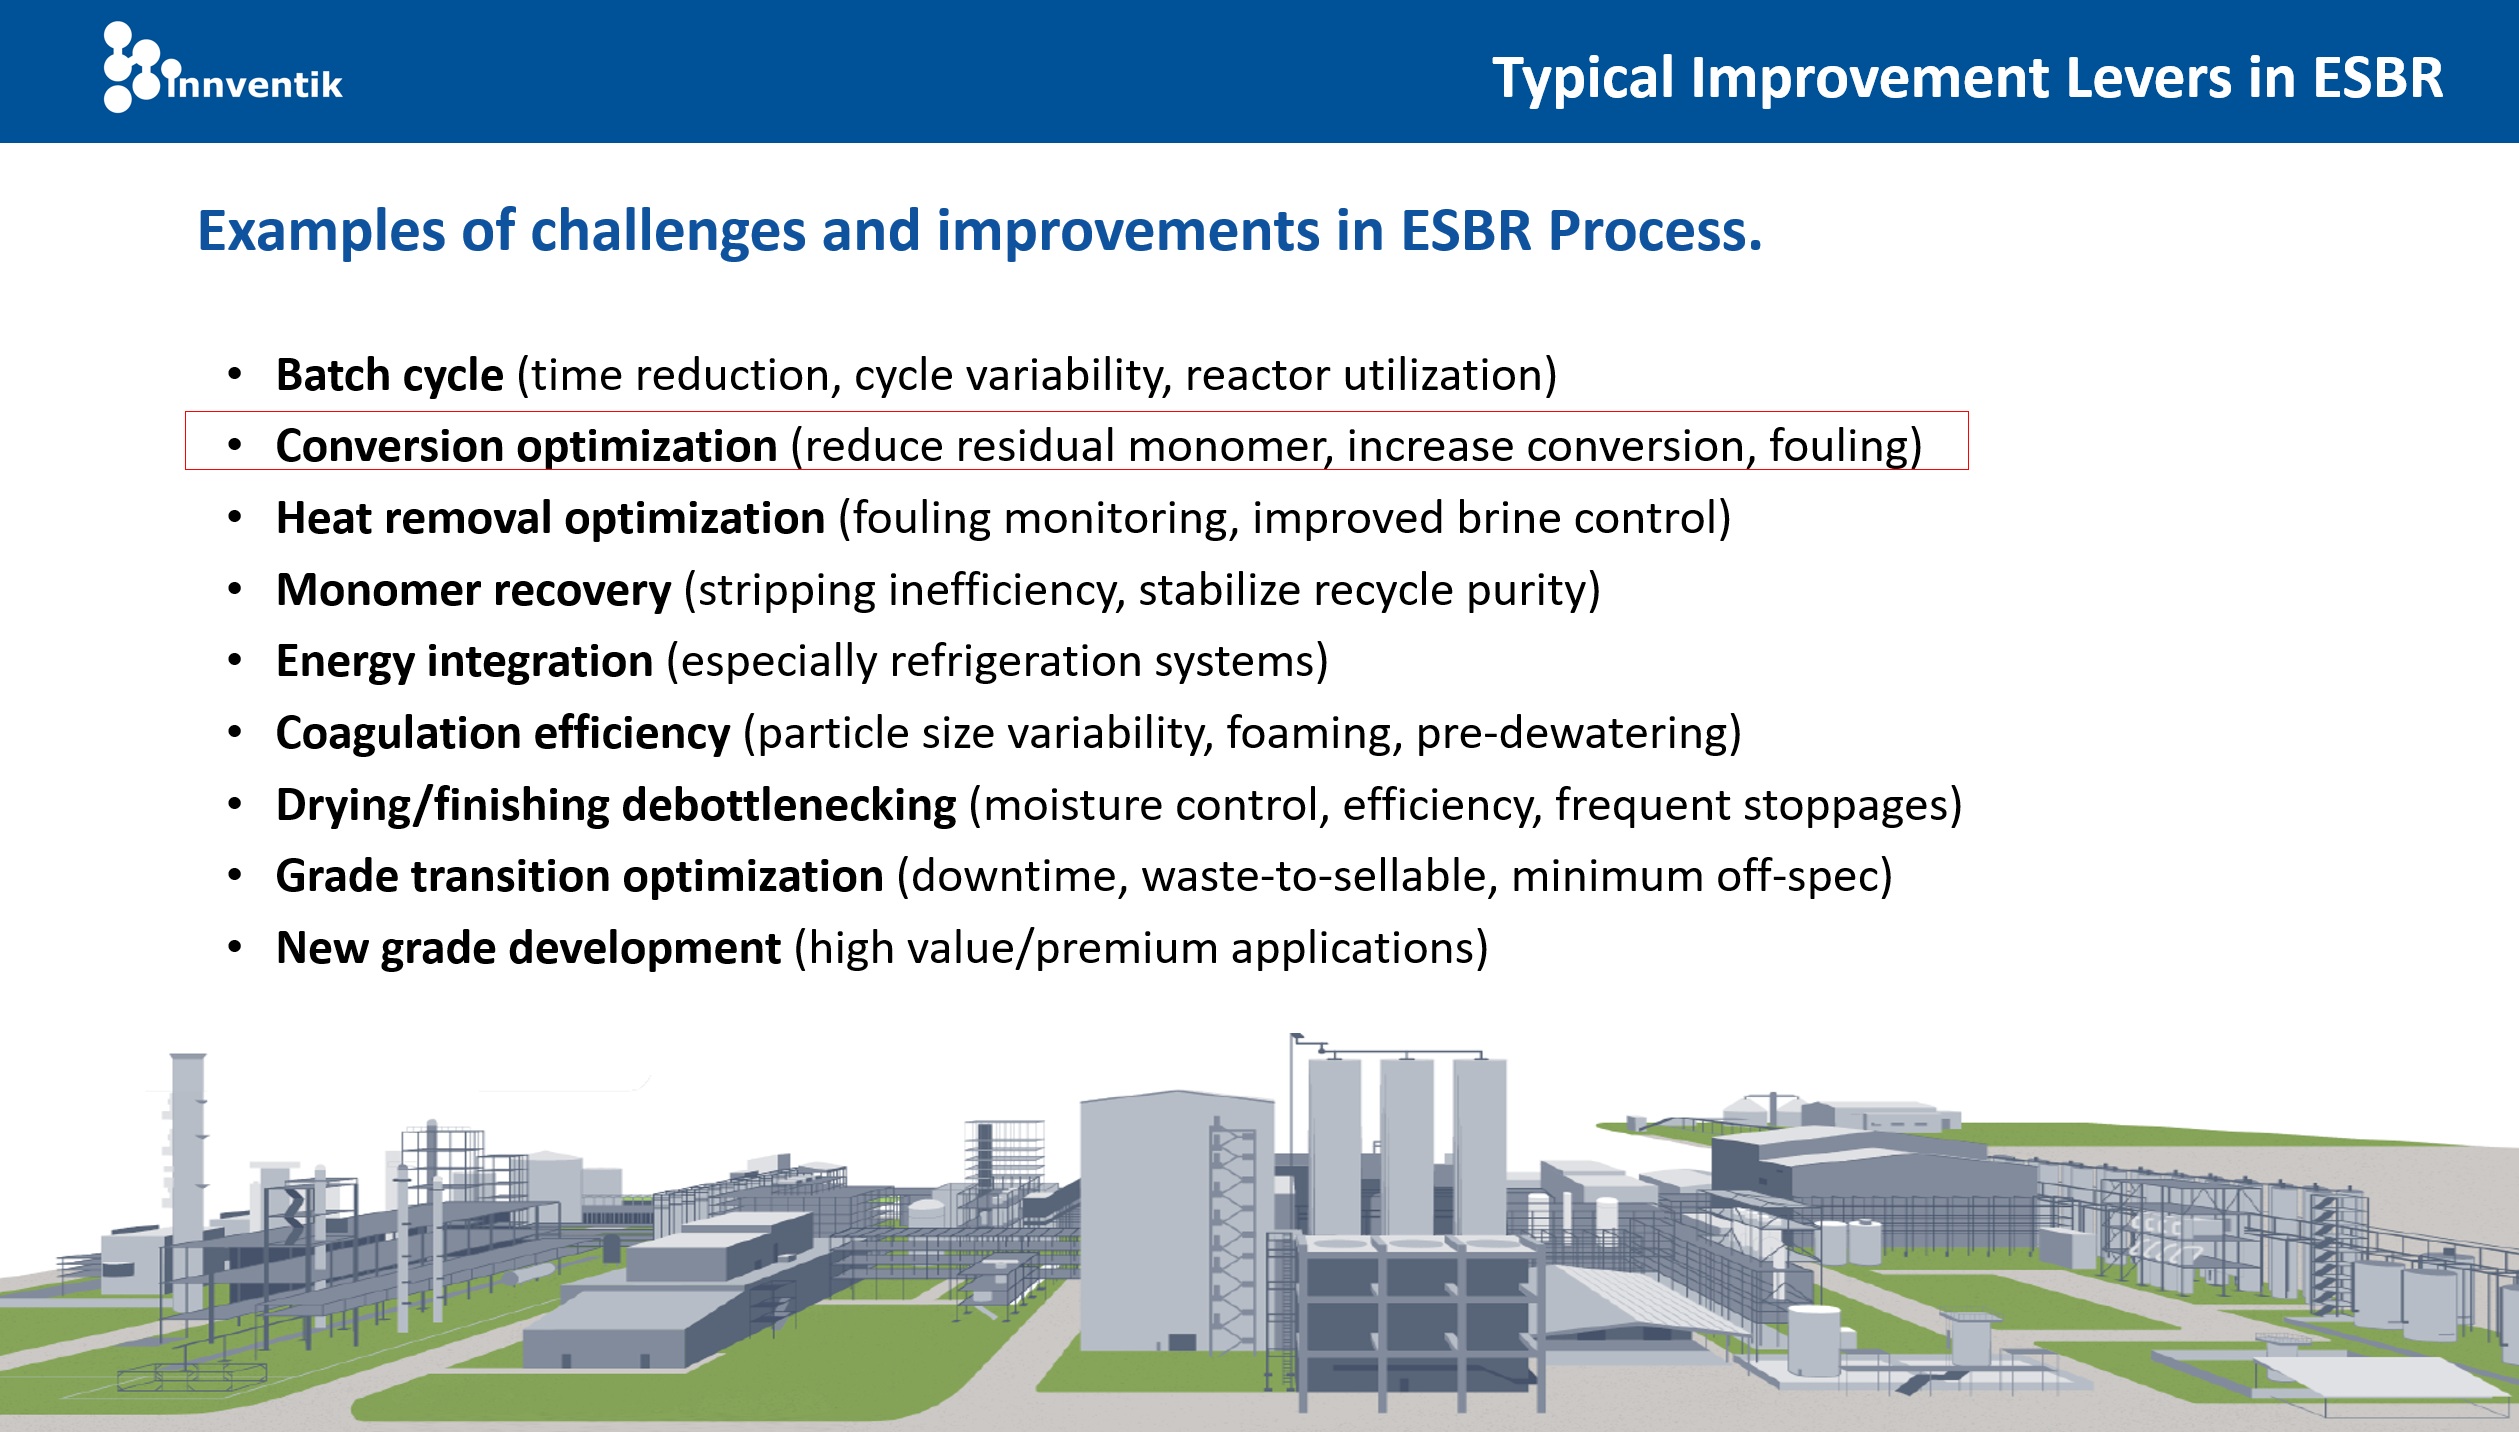
The specific improvement levers will depend on the configuration, product portfolio and operating history of each plant. Typical areas include batch-cycle reduction, conversion optimization, heat-removal performance, monomer recovery, refrigeration and energy integration, coagulation efficiency, drying and finishing debottlenecking, grade-transition optimization and new-grade development.
Innventik’s methodology starts by defining objectives, plant boundaries and KPIs. Historical production, quality and utility information is then combined with operating procedures, recipes, plant observations and discussions with operating personnel.
The process is mapped from raw materials through finished product, and actual performance is compared against expected or theoretical performance. Bottlenecks and losses are validated using plant data rather than assumptions.
Root causes are subsequently analyzed and potential improvements benchmarked against industry practice. Opportunities are quantified and prioritized according to impact and implementation effort, distinguishing relatively fast operational improvements from modifications requiring engineering or capital investment.
The result is an implementation roadmap, rather than simply a list of observations. The assessment methodology progresses from objectives and data collection through process mapping, performance analysis, bottleneck identification, root-cause analysis, benchmarking, opportunity identification, prioritization and recommendations.
Evolving existing ESBR assets
Many ESBR plants have operated successfully for decades. Their age does not necessarily mean that their fundamental technology needs to be replaced.
The opportunity is often to understand how the existing process actually performs today, identify the interactions limiting its performance, and selectively introduce better operating practices, process modifications, automation or advanced technologies where they generate demonstrable value.
For ESBR producers, this provides a practical route to extend the competitiveness of existing assets: reduce production cost, recover latent capacity, improve consistency and reliability, reduce environmental impact, and create the process flexibility required for differentiated products.
Author: Dr. Walter Ramirez, Managing Partner, Innventik S.L. (walter@innventik.com)
Catalyst and Initiator Residue Elimination in Solution Polymerization Processes
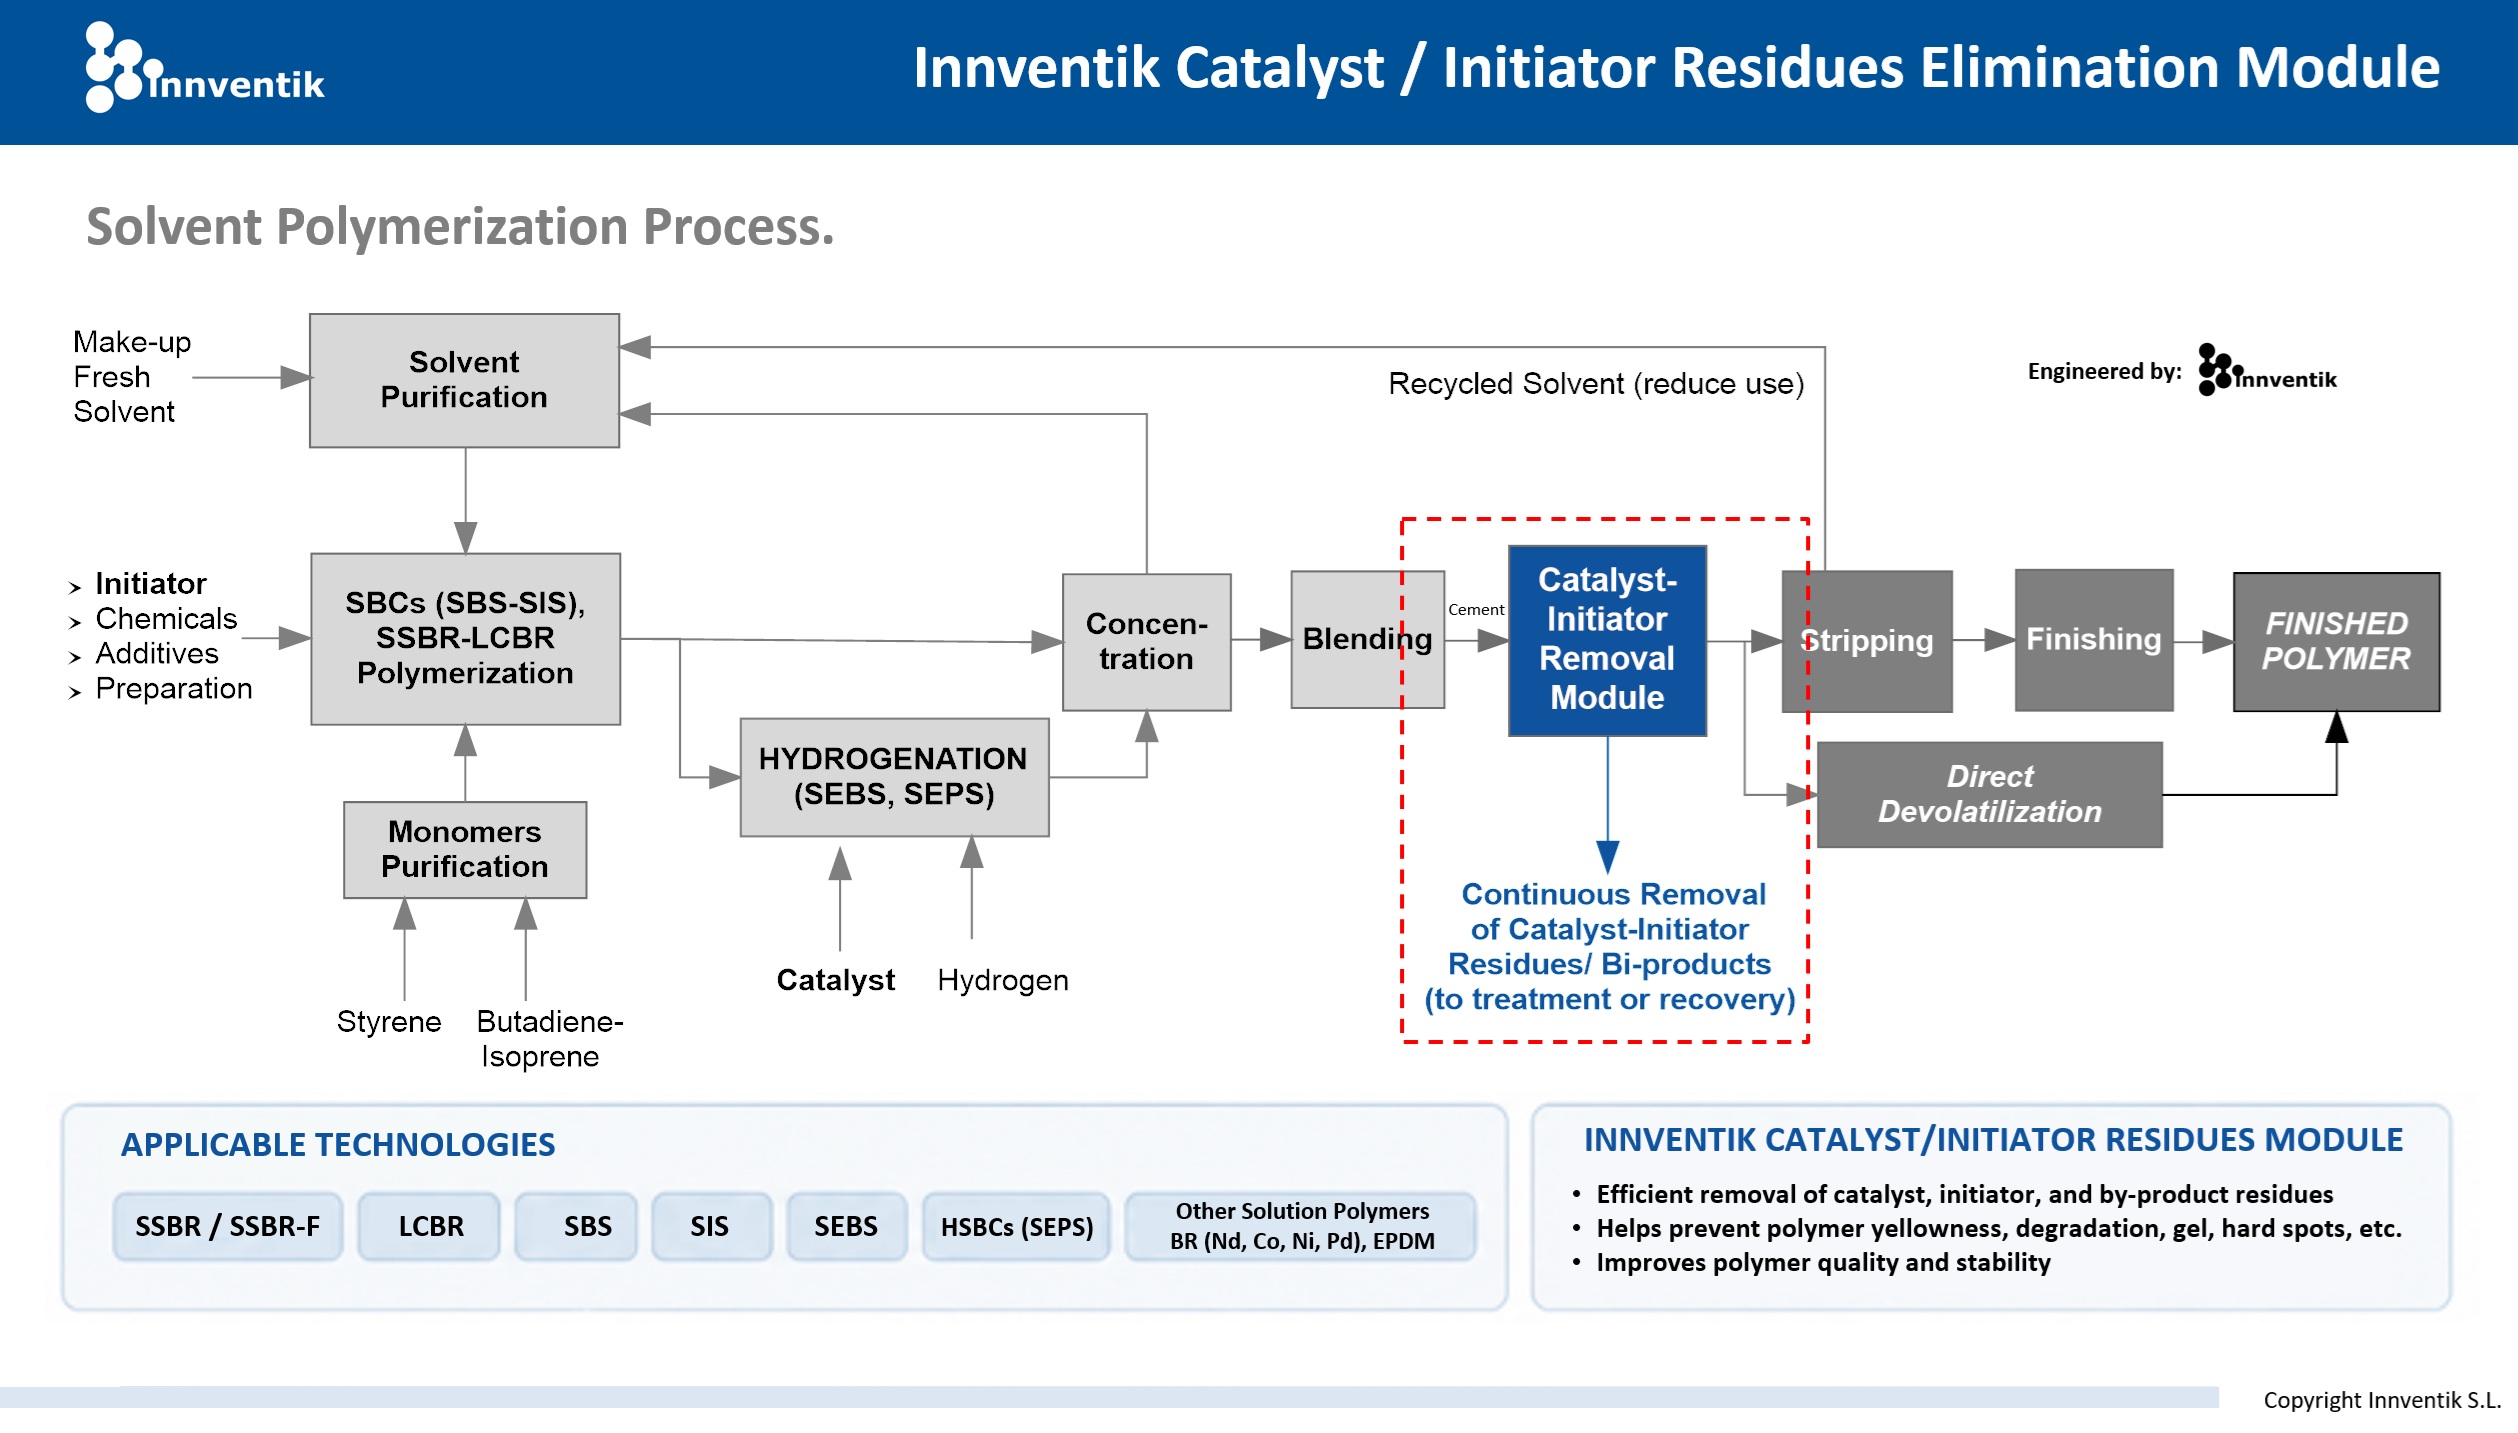
Solution polymerization technologies are widely used to manufacture high-performance synthetic rubbers, elastomers and specialty polymers, including SSBR, LCBR, SBS, SIS, SEBS and related materials such as BR (Ned, Co, Ni, Pd) or EPDM.
Depending on the polymerization chemistry, catalysts, initiators and associated reaction residues may remain within the polymer solution after polymerization. Their presence can become relevant to product purity, polymer properties, downstream processing and the ability to manufacture demanding specialty grades. The presence of catalyst and/or initiator residues may lead to polymer yellowness, degradation, and gel formation over time.
Residue elimination should be considered as part of the complete process
The optimum approach cannot necessarily be defined by considering polymerization alone. Polymer concentration, solvent system, reaction chemistry, polymer viscosity, downstream recovery technology and final product requirements all influence how a residue-elimination strategy should be designed and integrated.
INNVENTIK has developed a proprietary Catalyst & Initiator Residues Elimination Module intended for integration into solvent-polymerization processes.
The concept can be engineered and adjusted according to the specific polymer system and plant configuration and considered for both new facilities and existing-plant revamps.
Potential areas of application
The module can be implemented for batch, continuous and swing production configurations, before the and polymer recovery and finishing areas (Steam Stripping or Direct Devolatilization). The approach is particularly relevant to solution-polymerization technologies such as:
- SSBR and functionalized SSBR
- LCBR
- Styrene Block Copolymers (SBCs) such as SBS and SIS
- SEBS, SEPS and other hydrogenated block copolymers
- Other polymers manufactured through solvent-based polymerization processes (i.e EPDM)
An integrated engineering approach
Residue elimination from the polymer solution (cement) should be evaluated together with the surrounding process rather than as an independent operation. INNVENTIK’s approach therefore considers the complete manufacturing chain, including polymerization, solvent management and purification, polymer recovery, finishing, utilities and product-quality requirements. This allows the residue-elimination concept to be incorporated within broader process-improvement and industrialization programs.
Beyond conventional polymerization processes
The technology forms part of INNVENTIK’s broader development of advanced solution-polymerization concepts, including high-solids polymerization, batch-to-continuous processing flexibility, reduced solvent consumption, advanced polymer recovery and process intensification, integrating the most advance process practices for polymer recovery (direct devolatilization).
INNVENTIK supports projects from initial process assessment and feasibility evaluation through Conceptual, Basic and Detail Engineering, implementation, commissioning and start-up.
Companies interested in evaluating catalyst or initiator residue elimination in an existing or new polymerization process are invited to contact INNVENTIK for a confidential technical discussion.
Global Elastomers & Rubber Market 2026: Mid-Year Outlook
Madrid, Spain. July 3, 2026.
Global Elastomers & Rubber Market 2026: Mid-Year Outlook
The global elastomers and rubber industry enters 2026 with a mixed outlook: structurally resilient, but increasingly fragmented by region, geopolitics, and supply chain shifts.
Asia: Growth engine, but under pressure
Asia remains the center of gravity for both production and demand. China continues to dominate tire and synthetic rubber consumption, while Southeast Asia remains the key source of natural rubber. However, ANRPC reports natural rubber production fell 2.6% YoY in late 2025 due to adverse weather, tightening supply. At the same time, Chinese tire exports are under pressure from tariffs and anti-dumping measures, forcing producers to accelerate investments in Indonesia, Cambodia, and Vietnam.
Europe: Weak industrial demand, strong sustainability push
Europe remains soft in automotive and industrial elastomer demand, particularly in Germany and Central Europe. Energy costs and sluggish manufacturing continue to weigh on margins. At the same time, Europe is leading in circularity: pyrolysis, devulcanization, and bio-based feedstocks are attracting capital. Sustainability is no longer considered optional, it is one of the main investment drivers.
North America: Stable demand, reshoring gains
The US market remains relatively balanced, supported by replacement tires, industrial MRO, and infrastructure. However, trade barriers against Asian imports are reshaping sourcing strategies. More buyers are shifting toward Mexico and domestic compounding. Specialty elastomers (EPDM, silicone, HNBR) remain stronger than commodity grades.
India: Fastest industrial expansion
India is becoming the most dynamic growth market for elastomers. Tire capacity expansions, automotive growth, and infrastructure are driving both NR and SR demand. Local manufacturing incentives are accelerating investment in compounding, hoses, seals, and TPEs.
Russia & CIS: Supply risk remains elevated
The recent fatal incident at Sibur’s Nizhnekamsk synthetic rubber site highlights ongoing operational and supply risks in the region. While domestic demand remains steady, sanctions, maintenance challenges, and logistics constraints continue to create uncertainty for export-oriented material flows.
Market fundamentals
• Global rubber demand expected to reach 36.5 million ton by 2032 (+12%)
• 2025 demand growth estimated at +2.1%
• Natural rubber remains structurally tight
• Synthetic rubber margins remain volatile due to butadiene and energy swings
What does this means for business
This market cycle is not just about defending margins; it is a strategic window for transformation. With tighter raw material balances, higher safety expectations, and increasing sustainability pressures, this is the right moment for elastomer and rubber producers to revamp existing assets and invest in next-generation process technologies.
For converters, compounders, and OEMs, the priorities are secure supply, diversify sourcing, reduce energy intensity, prepare for tighter sustainability requirements.
For manufacturers, recent operational disruptions are a reminder of the importance of continuously investing in process safety, operational resilience, and material traceability, areas that are becoming critical competitive differentiators. The leaders will be the companies that act now to modernize their processes by:
- Reducing emissions and waste streams
- Improving energy efficiency
- Strengthening process safety systems
- Upgrading solvent recovery, degassing, drying, and polymer handling technologies
- Enhancing material traceability for faster and better decision-making
- Increasing plant flexibility and operational resilience
In today’s environment, process innovation is no longer just a technical upgrade; it is a business necessity. At Innventik, this is where we create value: helping industry take operations to the next level by reducing costs while improving safety, sustainability, and overall performance.
Sources: International Rubber Study Group (World Rubber Industry Outlook 2025–2032), Association of Natural Rubber Producing Countries (Monthly Statistical Reports 2025–2026), ICIS (feedstock and butadiene market analysis), Argus Media (energy and petrochemical pricing), and European Rubber Journal (industry and operational updates).
European Rubber Journal Recognizes Innventik’s Reactor Among Its Top 10 Sustainability Innovations
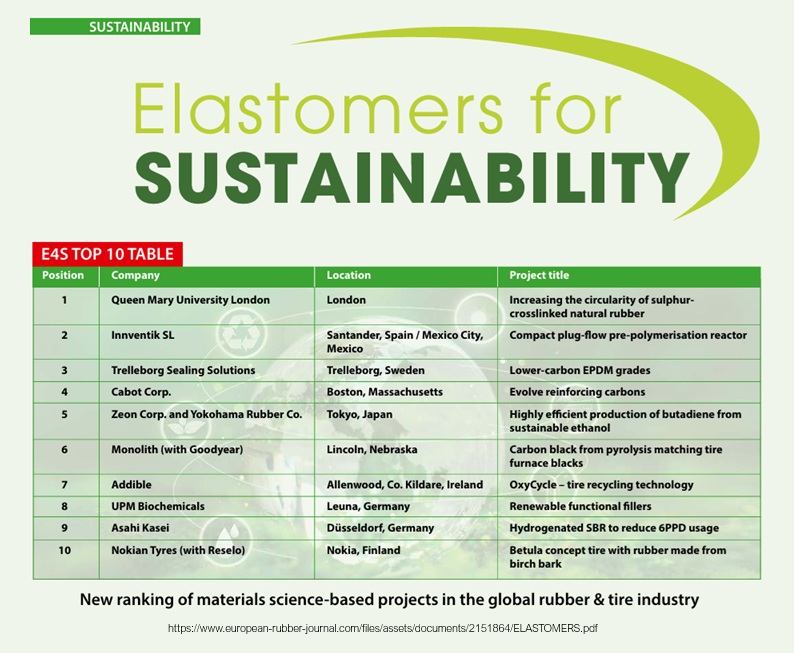
Santander, Spain – June 2026. Innventik is pleased to announce that its Compact Plug-Flow Prepolymerization Reactor has been recognized among the leading innovation projects in the global rubber and elastomer industry by the European Rubber Journal (ERJ). The technology was featured in the latest edition of ERJ’s prestigious Elastomers for Sustainability (E4S) Top 10 Projects Ranking, where Innventik achieved the #2 position worldwide among projects evaluated for their level of innovation, commercial potential, and contribution to sustainability. The recognition follows the recent publication of Innventik’s technical article, “Advancing Flexibility Between Batch and Continuous Elastomer Production,” authored by Dr. Walter Ramirez and Mr. Jorge Campos, which discusses how advanced reactor concepts can help address some of the most pressing challenges facing elastomer manufacturers today.
Addressing a Key Industry Challenge
The rubber and elastomer industry is under increasing pressure to improve sustainability, reduce emissions and energy consumption, increase operational flexibility, and deliver increasingly specialized materials with tighter quality specifications. Many synthetic rubber facilities continue to operate using technologies developed decades ago. While these processes remain robust, manufacturers are increasingly seeking new approaches capable of improving efficiency, flexibility, process control, and environmental performance. Innventik’s Compact Plug-Flow Prepolymerization Reactor was conceived to help address these challenges by providing a practical bridge between traditional batch polymerization and continuous manufacturing. The patented reactor concept is designed to stabilize the earliest and most sensitive stages of polymerization before the main reactor system, improving process robustness while minimizing disruption to existing production assets.
Advanced Reactor Technology
The reactor incorporates several innovative engineering features, including:
- Plug-flow reaction behavior with minimal back-mixing
- Controlled partial conversion and viscosity development
- High-efficiency heat transfer
- Dual agitation systems for mixing and self-cleaning
- Multiple injection points for monomers, initiators, solvents, and functionalization agents
Unlike conventional tubular reactors, the design combines high-performance mixing with self-cleaning capabilities, helping to reduce fouling, hot spots, and gel formation while improving heat and mass transfer. The technology was originally conceived for solution elastomer systems such as SSBR and LCBR but may also have applications in EPDM, specialty elastomers, and functionalized polymer systems.
Improving Flexibility Between Batch and Continuous Manufacturing
One of the key objectives of the reactor concept is to help bridge the operational gap between batch and continuous production. By stabilizing the most sensitive reaction stages and preconditioning the reaction mixture before entering the main reactor system, the technology may enable:
- Improved process consistency
- Enhanced operational flexibility
- Faster transitions between operating modes
- Reduced process variability
- Improved heat-removal performance
- Greater robustness during start-up and grade transitions
Rather than replacing existing reactors, the technology is intended to function as an enabling tool that strengthens process performance while leveraging installed assets.
International Intellectual Property Protection
The technology is protected by a growing international intellectual property portfolio, including:
- Granted Spanish Patent ES 2983867 B2
- International PCT Publication WO2025/221134 A1 (PCT/MX2025/050031)
- China Patent Application 202580003162.7
- US Patent Pending
These milestones reflect Innventik’s commitment to developing and protecting innovative technologies that create value for the global elastomer industry.
Recognition by the European Rubber Journal
The E4S ranking highlights projects that demonstrate excellence in innovation, commercialization potential, and sustainability impact within the rubber and tire sectors. The inclusion of Innventik’s Compact Plug-Flow Prepolymerization Reactor among the world’s leading sustainability-focused innovations represents an important validation of the technology’s potential relevance to future elastomer manufacturing.
Looking Forward
Innventik continues to engage with elastomer producers, technology developers, engineering companies, and research organizations worldwide to explore applications of the reactor technology and other advanced process innovations. As the industry seeks more sustainable, efficient, and flexible manufacturing solutions, Innventik remains committed to supporting the development of next-generation technologies for elastomers, polymers, and advanced materials.
Read the Full Article
“Advancing Flexibility Between Batch and Continuous Elastomer Production”
For more information regarding the technology, licensing opportunities, or technical collaboration:
Dr. Walter Ramirez
Managing Partner
Innventik S.L.
walter@innventik.com
From Laboratory Innovation to Industrial Reality: The Scale-Up and Industrialization Challenge
Innovation is the engine that drives industrial progress. Every year, universities, research centers, startups, technology developers, and industrial companies invest significant resources in the development of new materials, chemicals, polymers, biotechnology platforms, recycling technologies, energy solutions, and advanced manufacturing processes. Many of these innovations demonstrate excellent technical performance at laboratory scale and generate considerable excitement among researchers, investors, and potential customers.
Yet, despite their technical promise, only a small fraction of these technologies ever reach commercial deployment. The reality is that technological success in the laboratory does not automatically translate into industrial success. In fact, one of the greatest challenges facing innovators today is not invention, it is industrialization.
The Gap Between Innovation and Commercial Reality
The path from laboratory discovery to commercial production is often referred to as the “Valley of Death” of innovation. It is the stage where many promising technologies fail, not because they lack technical merit, but because they encounter significant obstacles during scale-up and commercialization.
A process that performs exceptionally well in a laboratory reactor may behave very differently at pilot, demonstration, or industrial scale. Heat transfer, mass transfer, mixing efficiency, residence time distribution, process control, product quality consistency, operability, safety considerations, raw material logistics, utility requirements, environmental compliance, and economics all become increasingly critical as scale increases.
What appears simple in a laboratory environment can become highly complex when translated into an industrial facility processing hundreds or thousands of kilograms per hour.
As a result, many organizations find themselves asking fundamental questions:
- What is the optimal process configuration at commercial scale?
- Which process steps represent the highest technical or operational risk?
- How should the technology be scaled to minimize investment risk?
- Is a pilot plant sufficient, or is a demonstration facility required before commercialization?
- What level of engineering is necessary to support investment decisions?
- What capital investment (CAPEX) and operating costs (OPEX) should be expected?
- What performance improvements are required to achieve commercial viability?
- How can investors, partners, or licensees be convinced of the technology’s value?
- What is the most efficient route to market?
- How can the technology be protected, licensed, and deployed globally?
The answers to these questions often determine whether a technology becomes a successful industrial business or remains a promising laboratory concept.
Industrialization Requires More Than Engineering
Successful industrialization is not merely an engineering exercise. It requires the integration of multiple disciplines, including:
- Process engineering
- Scale-up science
- Equipment and plant design
- Process safety
- Techno-economic analysis
- Investment evaluation
- Market assessment
- Commercialization strategy
- Intellectual property management
- Licensing and business development
The most successful projects are those that address these elements early and systematically, reducing uncertainty before major investments are committed. Organizations that develop a clear industrialization roadmap from the beginning are often able to reduce development timelines, lower technical risks, improve investor confidence, and accelerate market adoption.
Why Technology Scale-Up Matters
Technology scale-up is much more than increasing production volume. It is the process of translating laboratory knowledge into a reliable, safe, economically viable, and commercially attractive industrial operation. Ultimately, successful scale-up transforms innovation into industrial value. Proper scale-up enables companies to:
- Validate technical feasibility under industrial conditions
- Understand process limitations and operating windows
- Improve product quality and consistency
- Reduce operational and investment risks
- Generate reliable design data
- Optimize CAPEX and OPEX
- Strengthen investor confidence
- Accelerate commercialization
- Create a stronger foundation for licensing and global deployment
Technology Scale-Up & Industrialization at Innventik
At Innventik Consulting & Engineering, we support organizations throughout the complete journey from concept development to commercial implementation.
Our multidisciplinary team combines expertise in:
- Process Engineering
- Chemicals
- Polymers
- Elastomers and Rubber
- Advanced Materials
- Biotechnology
- Recycling Technologies
- Sustainable Industrial Processes
- Technology Commercialization
- Industrial Project Development
Our objective is straightforward: Reduce scale-up risks, accelerate commercialization, and transform promising technologies into successful industrial businesses.
Technology Scale-Up
Development of scale-up strategies, identification of critical process parameters, operating windows, equipment selection criteria, and industrial implementation roadmaps.
Pilot Plant Design
Design and engineering of pilot facilities used to validate process concepts, generate design data, optimize operating conditions, and support technology development.
Demonstration Plant Design
Engineering of demonstration facilities that bridge the gap between pilot operation and commercial deployment, validating operability, economics, product quality, and market readiness.
First Commercial Plant Engineering
Development of engineering packages for first-of-a-kind industrial facilities, reducing technical uncertainty and investment risk while supporting successful implementation.
Techno-Economic Evaluation
Assessment of process economics, profitability, sensitivity analysis, investment attractiveness, and commercialization pathways.
CAPEX & OPEX Assessment
Preparation of reliable investment and operating cost estimates to support strategic decision-making, fundraising activities, and investment evaluations.
Engineering Development
Comprehensive engineering services covering:
- FEL1 (Conceptual Engineering)
- FEL2 (Basic Engineering)
- FEL3 (Extended Basic Engineering)
- Detail Engineering
Licensing & Commercialization Support
Support in technology positioning, licensing strategies, partner identification, market entry planning, business development, and commercialization roadmaps.
Experience Across Multiple Industries
Innventik has supported industrial development projects across Europe, Asia, and the Americas in sectors including:
- Chemicals
- Specialty Chemicals
- Polymers
- Elastomers & Rubber
- Biotechnology
- Advanced Materials
- Renewable Fuels
- Recycling Technologies
- Sustainability Technologies
Our experience spans the full spectrum of industrial development—from process optimization and engineering design to technology scale-up, licensing support, and commercialization planning.
Turning Innovation Into Industrial Success
The journey from laboratory innovation to commercial reality is rarely straightforward. Technical challenges, engineering complexity, market uncertainty, and investment requirements must all be addressed before a technology can achieve industrial success. However, with the right strategy, engineering approach, and commercialization roadmap, these challenges can be transformed into opportunities. Because innovation creates value only when it reaches the market.
If your organization is evaluating a new technology, pilot plant, demonstration facility, licensing opportunity, or industrial scale-up project, Innventik would be pleased to discuss how we can support your path from innovation to industrial reality.
Madrid, Spain. May 27, 2026.
Reducing Cost, Improving Efficiency, and Increasing Competitiveness in Chemical & Polymer Plants
Madrid, May 18, 2026. The chemical, polymer, elastomer, and rubber industries are facing increasing operational and competitive pressure. Margins continue to tighten, energy and operating costs remain elevated, global competition from lower-cost regions is intensifying, and many industrial facilities are operating with aging assets and process limitations.
At the same time, producers are expected to:
- Improve productivity and operational efficiency
- Reduce OPEX and energy consumption
- Increase process flexibility
- Maintain product quality and consistency
- Develop differentiated products for higher-value applications
- Modernize operations without major CAPEX investments
These challenges are particularly relevant for medium and small producers seeking practical ways to remain competitive in increasingly demanding markets.
The Need for Practical Industrial Improvements
In many cases, significant opportunities for improvement already exist within current assets and operations. The challenge is not always the need for entirely new plants or disruptive investments, but rather identifying where inefficiencies, bottlenecks, operational limitations, and process instability are affecting performance.
Areas such as:
- Steam and solvent consumption,
- Reactor efficiency,
- Stripping and finishing operations,
- Process stability,
- Catalyst residues,
- Fouling,
- Yield losses,
- Operational consistency
can often be improved through targeted engineering assessments and implementation of advanced industrial process practices.
Innventik’s Approach
At Innventik Consulting and Engineering, we support chemical, polymer, elastomer, and rubber producers through practical engineering and industrial expertise focused on delivering measurable operational improvements and long-term competitiveness.
Our activities include:
- Process assessments, optimization, and debottlenecking
- Steam, solvent, and energy consumption reduction
- Yield and productivity improvement
- Troubleshooting of gels, color issues, consistency problems, fouling, and catalyst residues
- Reactor, stripping, and finishing enhancement
- Product differentiation and advanced grades support
- Batch, swing, hybrid, and batch-to-continuous process flexibility
- Conceptual (FEL1), Basic (FEL2), and Detail Engineering (FEL3)
Specialized Expertise Across Chemicals, Polymers, and Elastomers
Innventik works across a broad range of chemical and polymer technologies, including:
- SSBR
- Functionalized SSBR (SSBR-F)
- LCBR
- SBCs (SBS, SIS, SEBS)
- Styrenic polymers (ABS, HIPS, SAN and related technologies)
- Sustainable and advanced industrial process technologies
Our experience combines process engineering, troubleshooting, technology assessment, advanced materials understanding, and industrial implementation support.
Improving Existing Assets Without Massive CAPEX
Today, many producers are seeking alternatives to large greenfield investments. In this environment, maximizing the performance of existing assets becomes increasingly important.
Our focus is to:
- Reduce OPEX and energy consumption
- Improve the performance of existing assets
- Increase process reliability and operational consistency
- Integrate advanced industrial process practices
- Bring products and processes to the next level of competitiveness
In many cases, relatively focused process improvements can significantly improve productivity, consistency, flexibility, and profitability.
Looking Forward
The competitiveness of chemical and polymer producers will increasingly depend on their ability to modernize operations, improve efficiency, reduce operational risks, and develop differentiated products aligned with evolving market needs.
Industrial competitiveness today is no longer based only on capacity, but also on:
- Process efficiency,
- Operational flexibility,
- Product differentiation,
- Implementation of advanced industrial practices.
At Innventik, we believe many opportunities for improvement already exist inside current plants. The key is identifying them correctly and implementing practical, technically sound solutions effectively.
We would be pleased to exchange perspectives with companies evaluating opportunities to improve process performance, operational efficiency, and competitiveness in the chemical, polymer, elastomer, and rubber industries.
Innventik Celebrates 10 Years of Connecting Customers with Solutions

2026 marks a significant milestone for INNVENTIK: 10 years of connecting customers with solutions across the chemical, polymer, and rubber industries.
Madrid, January 2026. Founded with the vision of being a highly specialized engineering and consulting firm, INNVENTIK has built a strong reputation as a trusted partner for companies seeking practical, high-impact, and sustainable solutions in processes, products, and applications for Chemicals (Biochemicals, Phosphates, Fine Chimicals), Polymers (ABS, ABS-HH, MABS, MBS, HIPS, GPPS, SMA, SMMA), Elastomers, and Rubber and its applications (Adhesives & Sealants, High Performance Tires, Medical & Healthcare, Alimentary, Polymer Modification, Packaging, Polymer Blends & Alloys).

A Decade of Focused Expertise.
Over the past decade, Innventik has supported customers across Europe, Asia, and the Americas, delivering value through:
- Engineering & Process Assessments
Conceptual (FEL-1), Basic (FEL-2), and Detail (FEL-3) Engineering. Process Improvement, debottlenecking, troubleshooting, and optimization of Batch, Swing, Hybrid and Continuous Processes. - Advanced Polymer & Elastomer Technologies
Deep expertise in SSBR, LCBR, ESBR, NBR, and SBCs (SBS, SIS, SEBS), covering the full value chain (monomers & solvents purification, polymerization, solvent recovery, catalyst residue removal, tripping, finishing, and direct devolatilization). - Sustainable & Energy-Efficient Solutions
Implementation of best process practices to reduce OPEX, energy consumption, solvent losses, emissions, and operational risks, while improving product quality, consistency, productivity and plant flexibility. - Technology Services
Supporting innovation-driven projects with technology evaluation, licensing strategies, scale-up support, and investment risk mitigation.
- Business Development & Technology Scouting
Identifying customers, lead users, licensors, startups, research centers, and technology platforms worldwide to accelerate commercialization and growth.
Why Innventik Is the Right Choice
Innventik acts as a neutral, independent, and highly specialized partner, helping companies:
- Identify the best process technology options
- Improve performance of existing plants and assets
- De-risk investments through sound engineering and practical experience
- Implement solutions without compromising confidentiality or IP integrity
We leverage experience to deliver the next generation of sustainable processes, products, and solutions, helping our partners reduce costs and liabilities, achieve net-zero goals, and create long-term value.

Looking Ahead
As we celebrate our 10th anniversary, we remain committed to what defines Innventik: engineering excellence, integrity, and impact.
If your organization is facing technical challenges, evaluating new technologies, or looking to improve performance and sustainability, we would be pleased to explore how Innventik can support your goals.
Contact:
Dr. Walter Ramirez
INNVENTIK
Managing Partner, co-Founder
walter@innventik.com
www.innventik.com
🎄Merry Christmas and Happy New Year from the Innventik Team!🎄
As we close 2025, we would like to thank our partners and clients for the trust placed in Innventik. We look forward to 2026 with enthusiasm, ready to continue delivering innovative solutions in polymers, elastomers, and sustainable processes & technologies —together.
All the best!
Madrid, Spain, December 19, 2025.
Driving the Rubber and Elastomer Industry Towards Sustainability

Presented by Dr. Walter Ramirez at the IISRP AGM 2025
At the IISRP Annual General Meeting 2025 held in Ireland, Innventik’s Managing Partner and co-Founder, Dr. Walter Ramirez, delivered a keynote presentation on the pressing need for sustainable transformation in the rubber and elastomer industry. The session, titled “Driving the Rubber and Elastomer Industry Towards Sustainability: Materials, Processes, and Products”, outlined Innventik’s vision and actionable strategies for building a more responsible and future-ready industry.
The Call for Sustainability in Rubber & TPE
Global climate targets and policy frameworks such as China’s 2030–2060 climate roadmap and the European Union’s Green Deal are reshaping industrial practices. Companies across Asia, Europe, and North America are under pressure to adopt greener materials, improve energy efficiency, and integrate circular practices into their operations. Against this backdrop, Innventik outlined six key sustainability drivers:
-
Biobased Renewable Feedstocks
-
New Process Technologies
-
Sustainable New Products
-
Circularity & Recycling
-
Digital Transformation
-
Call to Action for Strategic Alignment
Enabling Sustainable Innovation
Dr. Ramirez presented breakthrough developments such as Innventik’s Plug-Flow Pre-Polymerization Reactor, ((Patent ES 2983867 B2) and international PCT filing (PCT/MX2025/050031), which enables the conversion of traditional batch processes into highly efficient continuous operations. This innovation improves reaction kinetics, reduces gel formation, minimizes color/yellowness, and shortens cycle times—delivering superior product quality and lower environmental impact.
Digital Intelligence for Sustainable Production
The presentation also introduced HYPPOS, Innventik’s real-time material tracking and analytics platform designed to optimize process performance. With AI-driven predictive modeling, digital twins, and smart traceability, HYPPOS enables manufacturers to reduce emissions, prevent off-spec production, and boost operational efficiency—key elements in meeting ESG goals.
Materials of the Future
Highlighting materials innovation, the presentation showcased sustainable options such as:
-
Kraft Lignin by Ligneasy: a renewable, high-performance filler for rubber and TPE compounds
-
PHAs by PHAST: medical-grade biopolymers that are biodegradable, biocompatible, and high-value
-
Bio-Butadiene Technologies: new methods using lignocellulosic sugars, 2,3-BDO, and bioethanol to replace fossil-based BD with lower CO₂ footprint
Strategic Priorities for Industry Leaders
Dr. Ramirez emphasized that the path forward demands:
-
Adoption of advanced process technologies to improve yield and cut emissions
-
Sourcing recycled and renewable raw materials
-
Implementing AI-based tools to optimize operations and traceability
-
Aligning policy, investment, and R&D to scale sustainable technologies
A Call to Collaborate
Innventik’s mission is clear: to empower the polymer and advanced materials industry with sustainable engineering, advanced technology, and expert consulting. Our multi-disciplinary team stands ready to collaborate with forward-thinking partners across the globe.
